Automated Sortation Systems for Warehouses
Our warehouse sorting systems deliver speed, control, and scalable accuracy.
Our warehouse sorting systems deliver speed, control, and scalable accuracy.
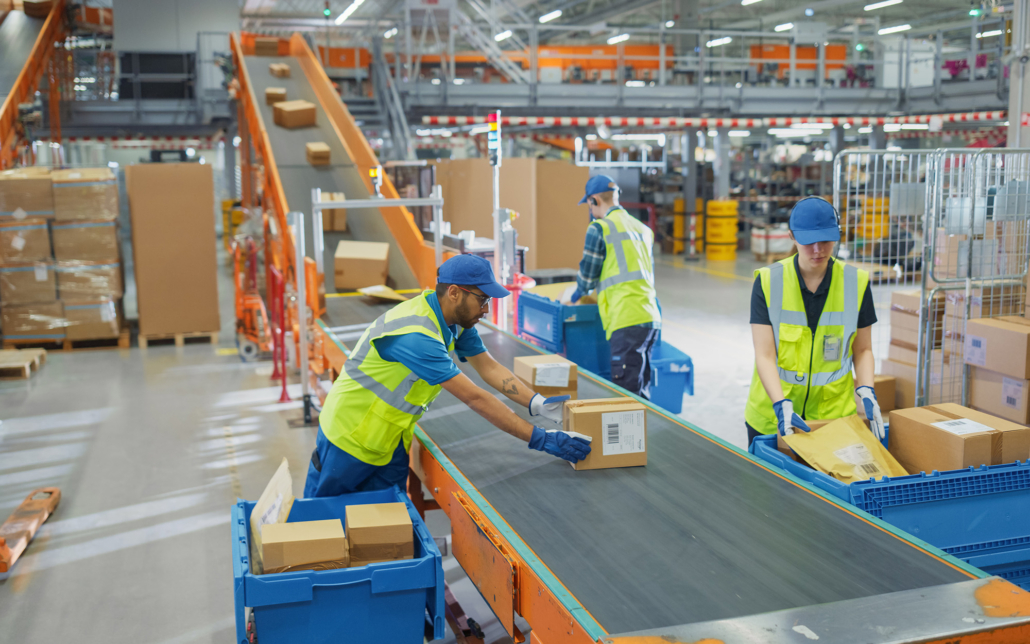
StorX designs and integrates automated sortation systems that route products accurately from picking through shipping. By directing items through defined, automated paths, our systems remove floor-level guesswork and hold throughput steady as order volume and complexity grow.
StorX designs sortation conveyor systems that route orders automatically, supporting high-speed sortation with consistent accuracy across shifts, zones, and order profiles.
StorX applies automated sortation conveyor systems that move products cleanly through each step, reducing rehandling, congestion, and the errors that slow fulfillment.
We deliver warehouse sorting systems with a turnkey approach that removes coordination gaps and shortens implementation timelines. You work with one partner accountable for design, integration, and performance.
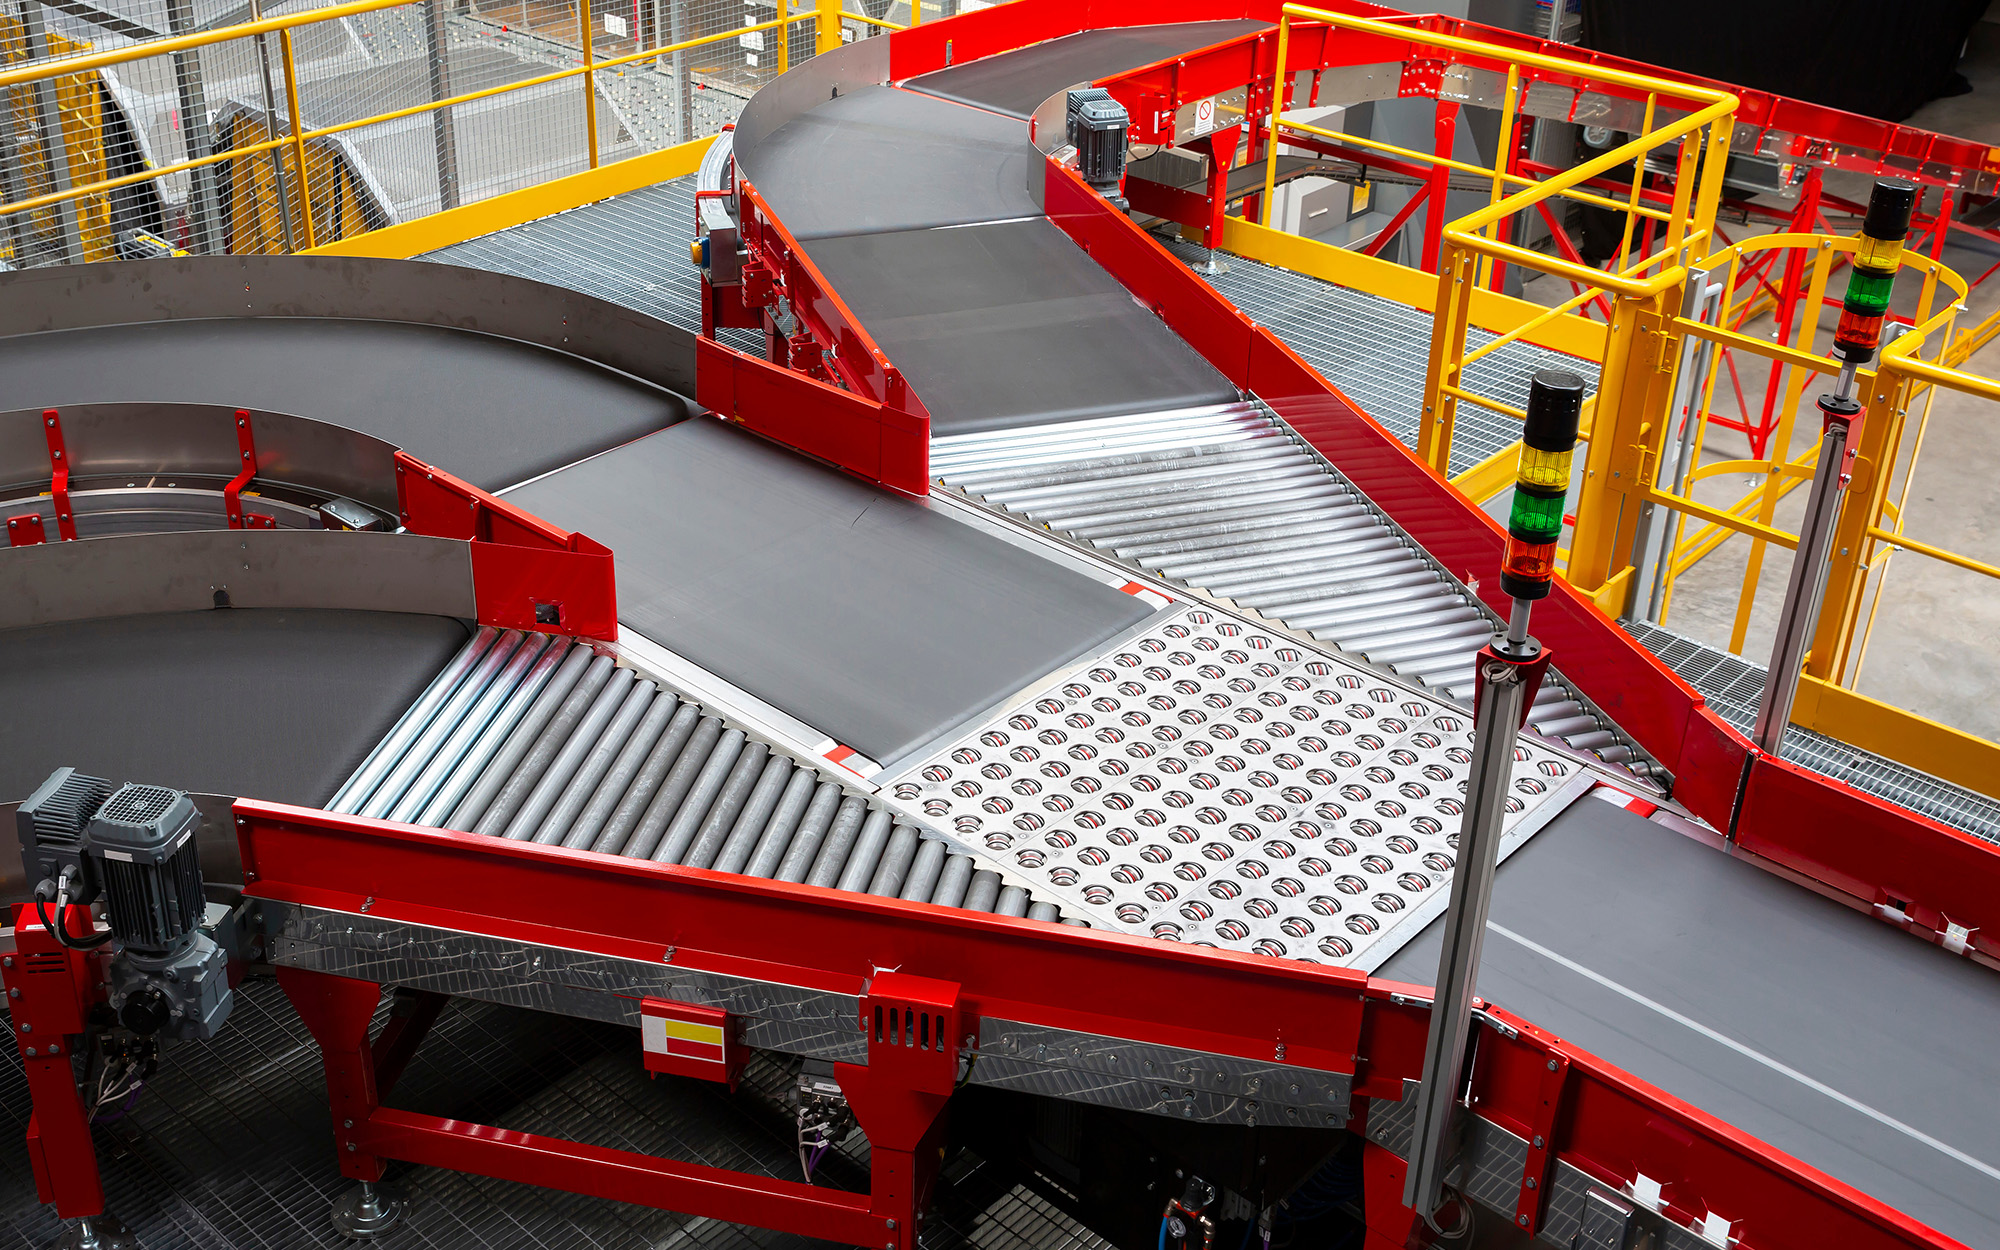
StorX engineers automated sortation systems around product mix, order profiles, and throughput targets. Using automated sortation conveyor systems such as belt conveyors, roller conveyors, and accumulation conveyors, we design solutions that support high-speed sortation without overwhelming downstream processes.
StorX integrates and installs systems with scanners, controls, and software so that sortation logic remains accurate as volume grows. These systems adapt easily, allowing you to add capacity, adjust routing strategies, and maintain control as operations evolve.
An automated sortation system uses scanners, controls, and conveyors to identify products and divert them to the correct lane, dock, or zone without manual handling. StorX builds conveyor-based sortation and selects the mix that fits your product mix, speed, and accuracy targets.
Belt conveyors move cartons, parcels, and loose items along a continuous belt, providing smooth, steady flow into and through the sortation process.
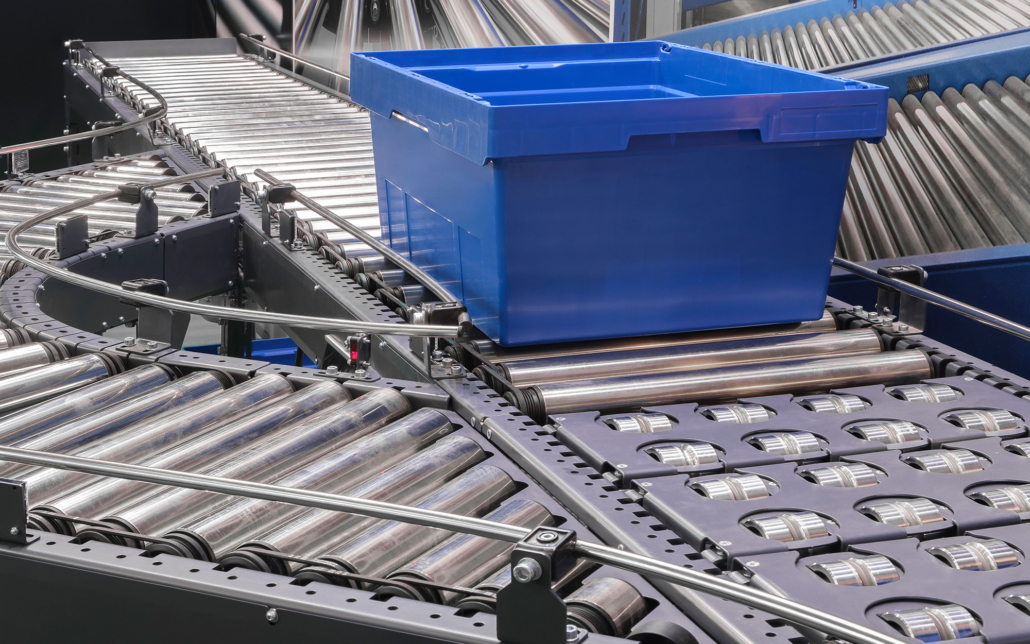
Roller conveyors use gravity or powered rollers to move cartons and totes, and they support diverting and routing along the sortation line.
Accumulation conveyors hold product in a controlled queue so items release into sortation at the right pace, which prevents congestion and keeps throughput steady.
Automated sortation systems support operations where products move quickly and accurately to many destinations. StorX designs and installs sortation systems for facilities across Atlanta, Texas, the East Coast, and beyond.
Sortation systems add the most value wherever high order volumes route to many destinations, including:
StorX supports industries where sortation drives speed and accuracy, including Retail and E-Commerce, Third Party Logistics, Food and Beverage, Manufacturing and Industrial, and Warehouse and Distribution.
An automated sortation system works in three stages. Induction feeds items onto the line at a steady rate, identification reads each item’s barcode, RFID, or dimensions to determine its destination, and the divert mechanism routes it to the correct lane, chute, or packing station. Control software ties the stages together so every item reaches the right place as volume scales.
Sortation systems add the most value wherever high order volumes route to many destinations, including:
Automated sortation systems make sense when manual sorting limits speed, accuracy, or scalability as order volume grows. StorX applies sortation conveyor systems where routing products automatically will lift throughput and reduce errors.
StorX designs conveyor-based sortation using methods such as sliding shoe, pop-up wheel, and roller diverters, matched to your product mix, speed, and accuracy targets.
Yes. StorX integrates warehouse sortation systems into existing layouts, equipment, and workflows, so you improve performance without a full facility redesign.
Yes. StorX delivers sortation systems through a turnkey model covering engineering, integration, and installation under one accountable partner.